
 English (NG)
 English
 Español
 Русский
 Português
 Bahasa Indonesia
 اردو
 বাংলা
 Español (MX)
 Tiếng Việt
 日本語
 한국어
 العربية
 Bahasa Melayu
 English (SG)
 Filipino
 ไทย
The Advanced Manufacturing Process for Our 125g 1/4 Club Tinplate Cans
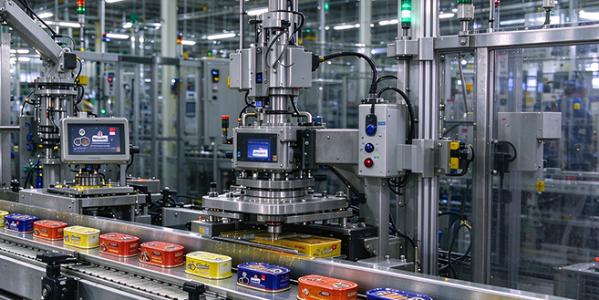
At GradeTinCans, every empty container is a product of rigorous mechanical precision and advanced metallurgy. Our automated, high-speed production lines turn premium steel coils into ready-to-fill, retort-safe food packaging through a seamless, 7-stage manufacturing process:
Step 1: Premium Coils De-coiling & Precision Slitting (Coil Uncoiling and Precision Slitting)
The manufacturing process begins with ultra-pure, cold-reduced Electrolytic Tinplate (ETP) coils sourced directly from top-tier mills like BAO STEEL and SHOUGANG. The giant steel coils are mounted onto automated de-coilers, straightened to eliminate stress memory, and then slit into precise, high-uniformity metal sheets calibrated to the exact gauge thickness required for drawn containers.
Step 2: High-Definition Offset Lithographic Printing & Coating (High-Precision Tinplate Printing and Inner Wall Coating)
Before mechanical forming, the flat tinplate sheets pass through our state-of-the-art multi-colour offset lithography lines.
- External Artwork: High-heat resistant, food-safe inks print your brand's customised design with crystal-clear dot reproduction. An external overprint varnish (OPV) is applied to protect the graphics from scratch damage during subsequent tooling.
- Internal Protection: The reverse side is evenly coated with premium, 100% BPA-free organic lacquers (such as organosols or epoxy-phenolic resins). The coated sheets travel through thermodynamic curing ovens to ensure complete chemical polymerisation, creating an impermeable barrier against acidic tomato sauces and aggressive brines.
Step 3: Cupping & First-Stage Shallow Drawing (Cupping and Primary Shallow Drawing)
- Because the 125g 1/4 Club can is a Two-Piece (2-Piece) container, it has no side seams or bottom welds, vastly minimising leakage risks. Coated sheets are automatically fed into high-speed cupping presses. Precision dies blank the metal into circular or rounded rectangular blanks and instantly perform the first shallow "draw," transforming the flat sheet into a seamless, low-walled metal cup.
Step 4: Secondary Rectangular Re-drawing & Ironing (Secondary Rectangular Re-drawing and Progressive Thinning Deep Drawing)
- To achieve the classic 1/4 Club rectangular geometry without tearing or fracturing the tinplate or internal lacquer, the cup undergoes a series of progressive re-drawing operations. Specialised forming dies carefully distribute the metal, stretching the walls upward while maintaining a perfectly uniform base thickness. The wall is ironed (thinned) to optimise material efficiency while retaining high crush resistance.
Step 5: Automated Edge Trimming & Flanging (Automatic Trimming and Flanging Process)
- As the cup is drawn to its final depth, the top edge remains uneven due to directional metal flow (earing). The raw cans enter an automated rotary trimmer that shears off the uneven top scrap with micron-level tolerance. Immediately following, the pristine top edge undergoes a flanging process, folding the lip slightly outward to create the perfect radius required for the client's double-seaming machinery.
Step 6: 100% Online Optoelectronic Leak Detection (100% Online Optoelectronic and Pressure Leak Detection)
- To guarantee zero-defect delivery to South-East Asian fish canneries, 100% of finished cans pass through our high-speed, online automated inspection block.
- High-Pressure Tester / Light Tester: Every single can is subjected to automated differential pressure testing and ultra-sensitive optoelectronic pinhole detection. Cans with even a sub-micron rupture, fracture or flange defect are automatically blasted off the line by pneumatic rejectors, safeguarding your packing lines from sealing failures.
Step 7: Automated Magnetic Palletising & Seaworthy Packing (Automated Magnetic Palletising and Heavy-Duty Export Packing)
- Flawless empty cans are picked up by automated magnetic palletisers, neatly aligned, and layered onto heavy-duty, heat-treated export pallets. High-strength plastic slip sheets are placed between each layer to avoid metal-on-metal friction. The entire pallet is then completely wrapped in multi-layer, heavy-gauge moisture-barrier stretch film, complete with top covers and rigid edge protectors, ensuring the cans arrive at your factory floor in sterile, rust-free and dent-free condition.